When a laser welding machine produces weaker seams, the problem rarely begins with one dramatic failure. It often appears as a smaller melt pool, slower penetration, or rougher bead edges. Operators may ask, “why is my laser welding machine losing power output,” especially after hours of stable production. That question deserves measured testing, not guesswork. A dirty protective lens, unstable cooling, incorrect focus, or aging optical components can reduce energy at the workpiece. Power shown on the control panel may differ from power delivered through the optics. It is easy to blame the laser source too quickly. Sometimes, the real cause is maintenance history.
This guide approaches the issue from a technician’s perspective, using observable symptoms and manufacturer-approved checks. We will connect weld appearance with beam alignment, coolant temperature, gas flow, lens condition, and electrical stability. Simple records matter. Note the material, thickness, settings, ambient temperature, and operating time. These details can expose gradual drift that one test misses. Do not touch optics or open energized equipment without proper training and isolation procedures. A calibrated power meter provides stronger evidence than visual judgment alone. Even experienced operators can misread a contaminated lens as a software fault. That mistake costs time. The diagnosis may remain uncertain until measurements confirm it. Reliable troubleshooting protects the machine, the operator, and weld quality while narrowing each possible cause.
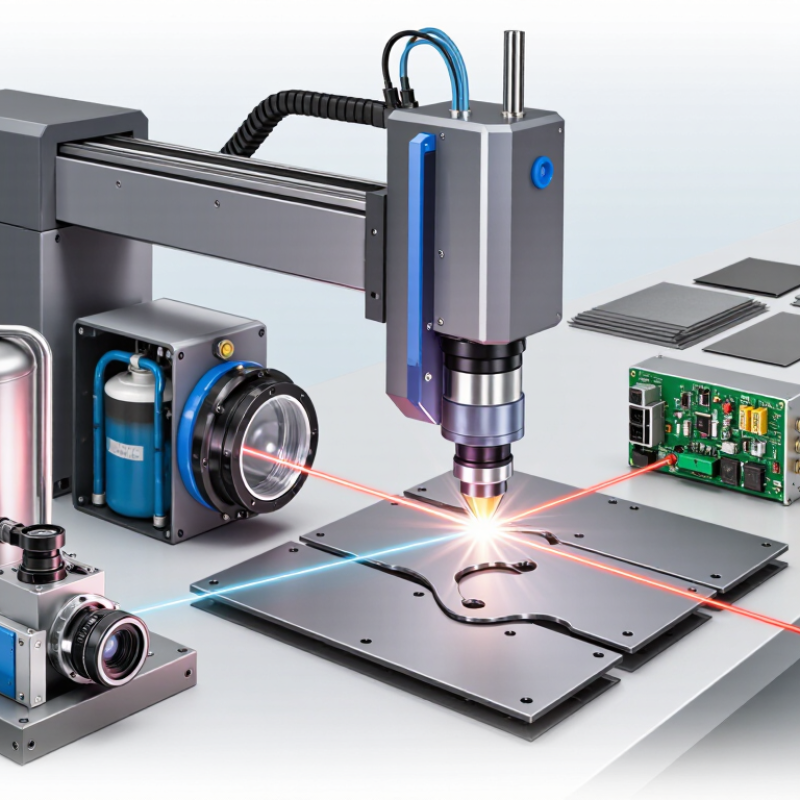
Laser welding power loss should be defined with measured watts, not visual impressions. Set the machine to 1,000 W, then measure actual output at the work position. If the meter reads 860 W, the absolute loss is 140 W. The loss rate is 14 percent. This comparison gives technicians a clear starting point.
Use a calibrated power meter suitable for the laser wavelength and power range. Let the machine complete its normal warm-up cycle before testing. Record the setpoint, measured output, date, operating time, and test location. A dirty protective window, misaligned optics, unstable cooling, or a damaged fiber can reduce delivered power. Check the reading twice. Small changes matter.
Do not blame the source too quickly. I once treated a low reading as a source failure, but the meter connection was poor. The real problem was simpler. Measure at the same point each time. Compare cold and warm readings. If 1,000 W produces 980 W one day and 840 W later, the trend deserves attention. Confirm the meter with a known reference when possible. Also inspect cooling temperature, alarm history, beam path condition, and connector cleanliness. A low setpoint can hide a normal machine, while an inaccurate meter can create a false fault. Document every adjustment, even the unsuccessful ones. Those records often reveal whether power loss is sudden, gradual, or caused by test conditions.
Define power loss by comparing the programmed setpoint with the measured optical output in watts.
The measured output is below the programmed setpoint in every test. Power loss is calculated as Setpoint − Measured Output, while the loss percentage is (Setpoint − Measured Output) ÷ Setpoint × 100. In this example, the loss increases from 3.0% at 500 W to 13.3% at 1,500 W, which may indicate contamination, optical misalignment, cooling issues, or a declining power source.
When a laser welding machine loses power, check the measured output before changing process settings. The common reference is a ±5% output-tolerance range. Record the reading at the same power, pulse width, and operating temperature. Use a calibrated power meter, and compare results with the machine’s original baseline.
A gradual decline beyond 5% may indicate laser source aging, especially when weld penetration becomes shallow or cycle times increase. However, aging is not the only explanation. Contaminated optics, poor fiber coupling, unstable cooling, and incorrect meter calibration can create similar symptoms. A clean lens can make a surprising difference.
Measure it twice.
Then inspect the cooling system, beam path, and electrical supply.
In practical maintenance work, technicians sometimes blame the source too early. I have seen a dirty protective window produce a false aging diagnosis. The ±5% range is helpful, but it is not a final verdict.
If readings remain below tolerance after cleaning and verification, request a qualified service evaluation. Keep dated output records, because a slow decline is easier to confirm than a single abnormal reading.
A laser welding machine can appear mechanically healthy while its power at the workpiece quietly declines. For systems operating around 1,030–1,080 nm, inspect every optic in the beam path. The protective window, collimation lens, focusing lens, and delivery fiber end are common loss points. Even a thin film of metal vapor can absorb energy, scatter the beam, and create local heating.
Start with the power meter, not visual brightness. Record output at a stable setting, then compare it with the machine’s normal baseline. Power down safely before inspection. Use suitable illumination to check for haze, specks, fingerprints, or a brownish coating. Never touch an optical surface directly. A contaminated window may look acceptable from one angle. It may fail under focused light.
Clean only with procedures approved for the optic’s coating. Use clean, lint-free materials and a compatible solvent. Do not reuse swabs. After cleaning, measure the output again and document the change. A small improvement confirms transmission loss, but it does not prove the entire system is healthy. I have seen operators replace a lens when the real issue was contamination inside the beam delivery path. That mistake costs time. It also creates a new alignment risk. If transmission remains low, check connector seating, beam alignment, cooling, and source stability with qualified service personnel.
Why Is My Laser Welding Machine Losing Power Output?
A falling weld result does not always mean the laser source is failing. In many cases, the beam reaches the workpiece with poor alignment, incorrect focus, or an enlarged spot. Check the beam at the 0.1 mm scale. A small shift can move the focal point beyond the joint, especially on thin materials.
ISO 11146-1 defines beam-width measurement using second-moment methods, which help verify whether the beam remains properly shaped. Measure beam position before adjusting power. Then inspect the focal plane with a calibrated beam profiler or approved test target. Record the spot diameter, not only the machine’s displayed power. A 0.20 mm spot becoming 0.30 mm reduces energy density by about 56%, assuming equal power and a circular profile. That difference is substantial.
Keep the optics clean and confirm the protective window is seated correctly. Even slight contamination can distort the beam and shift the apparent focus. The 2024 World Robotics report recorded 542,000 industrial robot installations worldwide during 2023. More automated welding cells make repeatable optical checks increasingly important. However, a report is not a diagnosis. I have seen operators increase power before checking focus, which often worsened spatter and heat spread. Verify alignment at low-risk settings, compare measurements with maintenance records, and repeat the test after thermal stabilization. The first reading may be wrong.
| Diagnostic Dimension | Verification Method | Typical Acceptance Reference | Example Reading | Status | Corrective Action |
|---|---|---|---|---|---|
| Measured laser output power | Measure with a calibrated power meter after warm-up, using the same operating mode and duty cycle as production. | Within ±5% of the programmed or documented baseline. | Baseline: 2,000 W Measured: 1,720 W Deviation: −14% |
Fail | Repeat the measurement at the source and at the processing head to isolate internal, delivery-path, or head-related losses. |
| Beam-axis alignment at the nozzle | Place a low-power burn paper, target card, or camera target at the nozzle exit and compare the beam center with the mechanical axis. | Beam-center deviation no greater than 0.10 mm from the nozzle axis. | 0.18 mm offset toward the 3 o’clock position | Fail | Inspect and adjust steering optics, head seating, and mounting interfaces. Recheck at multiple working distances. |
| Focal-plane position | Perform a controlled z-height sweep and record the smallest stable spot or highest process response. | Actual focal plane within ±0.10 mm of the programmed work position. | Actual focus: +0.30 mm above programmed position | Fail | Verify the z-axis reference, workpiece height, lens seating, and focal-offset settings before recalibration. |
| Focused spot diameter | Measure the focused spot using a suitable beam profiler or validated burn-pattern method at the work plane. | Within ±10% of the established process baseline; confirm at the 0.10 mm scale. | Baseline: 0.40 mm Measured: 0.56 mm Increase: 40% |
Fail | Check focus position, protective optics, beam quality, and contamination. Do not compensate by increasing power until the spot is verified. |
| Spot position relative to the joint | Use a crosshair target or test weld to compare the beam center with the seam centerline. | Beam center within ±0.10 mm of the intended joint location. | 0.12 mm lateral displacement | Check | Correct fixture registration, teach-point position, or optical alignment. Confirm at the start and end of the travel path. |
| Beam-profile symmetry | Review the beam profile at or near focus with a calibrated profiler; compare major and minor axes. | Ellipticity typically no greater than 1.20:1 for a stable circular process spot. | Major axis: 0.62 mm Minor axis: 0.42 mm Ratio: 1.48:1 |
Fail | Inspect optical surfaces and alignment. Confirm that no optic is tilted, damaged, loose, or thermally distorted. |
| Protective-window transmission | Inspect the window for haze, spatter, cracks, or coating damage and compare power before and after replacement with controlled settings. | Transmission loss should remain below 5% versus a clean reference window. | Estimated loss: 8.5% Visible brown deposit present |
Fail | Replace the window using the approved handling procedure, then repeat power, focus, and spot-size measurements. |
| Nozzle concentricity and standoff | Check nozzle runout with a gauge and verify the nozzle-to-work distance with a calibrated height reference. | Nozzle runout ≤0.10 mm; standoff within ±0.20 mm of the process setting. | Runout: 0.16 mm Standoff error: +0.25 mm |
Check | Clean the seating surface, replace a distorted nozzle, and reset the working distance before evaluating weld quality. |
| Shielding-gas flow at the nozzle | Measure actual flow at the nozzle outlet rather than relying only on the regulator or software setpoint. | Actual flow within ±10% of the qualified process setting and free from turbulence or blockage. | Setpoint: 15 L/min Measured: 11.8 L/min |
Check | Inspect tubing, filters, solenoid valves, nozzle blockage, and leaks. Reconfirm flow after maintenance. |
| Power stability during a 60-second test | Log output power continuously at a fixed setpoint after warm-up and calculate peak-to-peak variation. | Peak-to-peak variation no greater than 3% during a stable operating interval. | Variation: 6.2% Output falls after 35 seconds |
Fail | Check cooling temperature, interlocks, electrical supply, source alarms, and thermal lensing in the delivery optics. |
| Test-weld penetration response | Run a repeatable coupon weld with fixed power, speed, focus, shielding gas, and material thickness; measure cross-section penetration. | Penetration and bead width within ±10% of the qualified baseline. | Penetration: 0.62 mm vs. 0.82 mm baseline Reduction: 24% |
Fail | Complete optical checks first; then verify travel speed, material fit-up, surface condition, and parameter records. |
When a laser welding machine loses power, the chiller deserves attention before the laser source is blamed.
A typical coolant setpoint sits around 20–25°C. However, the displayed temperature may not reflect actual heat conditions inside the loop.
Run the machine under a normal welding load, then watch coolant temperature for ten minutes.
Record the inlet and outlet readings, not only the controller display. A rising outlet temperature can indicate restricted airflow, a blocked filter, or insufficient cooling capacity. Check the pump sound and coolant flow indicator. Weak flow matters.
Keep the chiller away from dust, walls, and direct sunlight. Clean the air intake carefully, because a thin dust layer can reduce heat exchange. Confirm the coolant level and inspect hoses for kinks or small leaks. The setpoint alone proves very little.
I once trusted a stable 22°C reading, while a partly blocked filter caused temperature spikes during longer welds. That assumption was wrong.
Compare performance at 20°C, 22°C, and 25°C, if the machine manual permits those settings. Let each condition stabilize before recording output power. Use the same material, duty cycle, and optical setup during every test. Otherwise, the results can mislead you.
Remember that room temperature also changes chiller performance. A unit working well in a cool workshop may struggle beside a hot welding enclosure. If temperatures remain unstable, have a qualified technician check sensors, refrigerant performance, and flow protection circuits.
Compare the machine setpoint with measured output at the work position. Set 1,000 watts and measure the delivered power. An 860-watt reading means 140 watts of absolute loss. That equals a 14% loss rate.
Use a calibrated power meter matching the laser wavelength and power range. Complete the normal warm-up cycle first. Record the setpoint, output, date, operating time, and test location. Measure twice.
A common reference range is ±5% of the expected output. A gradual decline beyond 5% may suggest source aging. Shallow weld penetration can support that suspicion. It is not proof.
Dirty protective windows, poor fiber coupling, and misaligned optics can reduce delivered power. Unstable cooling may cause similar symptoms. An inaccurate meter can create a false fault. Check simple causes first.
Measure at the same location, power level, pulse width, and temperature. Confirm the meter with a known reference when possible. Compare cold and warm readings. Small changes matter.
A typical coolant setpoint is around 20–25°C. The display may not show actual loop conditions. Measure inlet and outlet temperatures during normal welding. Watch the system for ten minutes.
Restricted airflow, blocked filters, weak coolant flow, and kinked hoses can cause temperature instability. Dust on the air intake reduces heat exchange. Check the pump sound, coolant level, and flow indicator. Weak flow matters.
If permitted, test at 20°C, 22°C, and 25°C. Let each setting stabilize before recording output power. Use the same material, duty cycle, and optical setup. Otherwise, results may mislead you.
Keep dated output readings and document every adjustment, including unsuccessful ones. Record cooling temperatures, alarm history, beam condition, and connector cleanliness. A gradual decline is easier to confirm than one abnormal reading. I once blamed the source too quickly.
If you are asking, “why is my laser welding machine losing power output,” start by comparing the programmed power setpoint with the actual measured output in watts. A difference may indicate source aging, calibration drift, or an issue in the delivery system. Check whether the laser source remains within the common ±5% output-tolerance range. If the reduction exceeds this range, further testing or professional servicing may be needed.
Next, inspect the 1,030–1,080 nm optical path for dust, residue, scratches, or contamination that can reduce transmission. Verify beam alignment, focus position, and spot size, especially when precision near 0.1 mm is required. Finally, confirm that the chiller is operating consistently around the typical 20–25°C setpoint. Excessive temperature variation can affect laser stability and gradually reduce welding performance.
Jigsaw Machine