Crooked marks rarely come from one careless setting. They usually reveal a mismatch between the laser beam, the workpiece, and the motion system. If you are asking, “why does my laser marking alignment look crooked,” inspect the entire marking path before changing speed or power. A tilted fixture, loose rotary attachment, dirty lens, or incorrect focal height can shift lines visibly. Even a small angle becomes obvious across a large metal plate.
Dr. Reinhart Poprawe, a respected laser technology expert and former director of Fraunhofer ILT, has emphasized a valuable principle: “Laser precision depends on controlling the entire process, not merely the beam.” That principle guides this 2026 troubleshooting overview. It focuses on practical checks, including frame squareness, gantry backlash, lens seating, software scaling, and workholding pressure. Use a test grid first. Watch how a 50-millimeter square changes at different positions. Record the error. Do not rely on appearance alone.
Some problems are easy to miss. A clean lens may still sit incorrectly. A rigid fixture may still hold the part at an angle. Your first diagnosis may be wrong. That is normal. Careful alignment requires patience, measured evidence, and repeatable adjustments. This guide explains how to identify the real source of crooked laser marking alignment and restore consistent results without guessing.
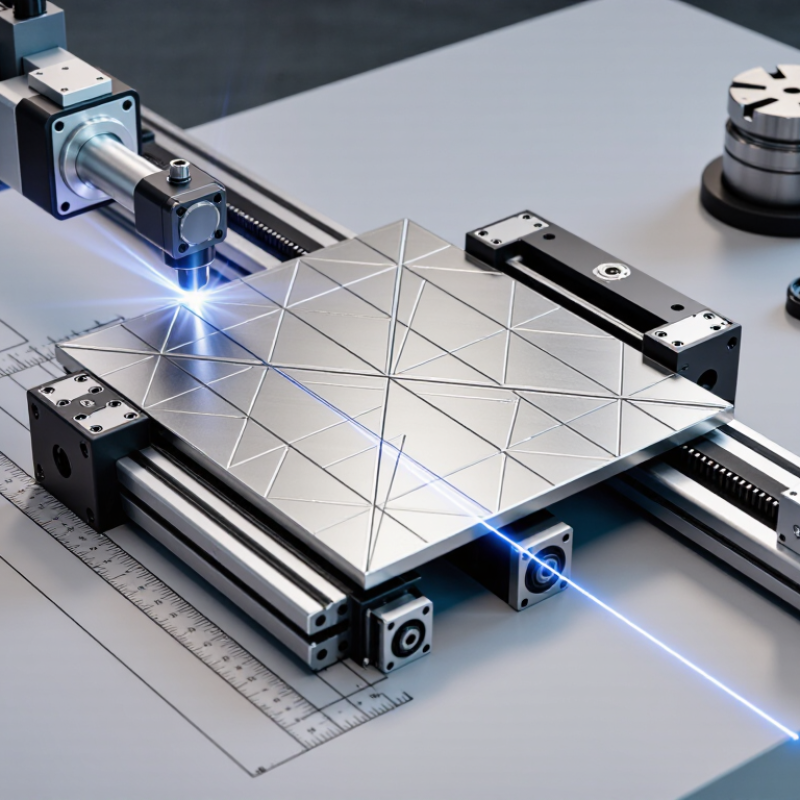
Crooked marking often starts with the workpiece, not the laser source. A loose fixture can shift during scanning. Even a small movement changes the marking angle. Check the part against the fixture stops before adjusting software settings. Dust, oil, or uneven surfaces can also prevent stable positioning.
Inspect the focusing distance across the entire marking area. A tilted part may look aligned near one corner but drift elsewhere. Lens contamination, thermal expansion, or a misaligned optical path can create similar patterns. In practice, a test grid reveals more than a single sample. Measure its spacing with calipers. Do not trust appearance alone.
Software scaling and rotation settings deserve careful review. Incorrect field dimensions may produce consistent, crooked results. A rotary attachment can introduce errors when its axis is not centered. Run a low-power outline before production. Record the fixture position, focus height, temperature, and correction values. This record supports repeatable troubleshooting and helps a qualified technician verify calibration. One overlooked detail remains common: the material itself may warp after heating. A clean first test can still mislead. Recheck alignment after several cycles.
Crooked laser marking often begins with a small alignment error, not a software failure. In 2026, inspect the laser head, fixture, and workpiece as one positioning system. A visible reference line helps reveal whether the beam exits squarely. Place a calibrated test plate beneath the head, then mark a small grid at several heights. If the grid shifts or widens unevenly, check the lens mount, focusing distance, and head stability. Dust on the optical window can also distort the mark.
The fixture deserves equal attention. A loose clamp may move only a fraction of a millimeter, yet letters can look noticeably slanted. Tighten each contact point evenly and check the base with a machinist’s level. Use locating pins or hard stops when repeatability matters. Soft pads can compress differently. That detail is easy to miss. Measure the fixture after several production cycles, because heat and vibration may change its position.
The workpiece must sit flat and against the same datum every time. Remove chips, oil, and burrs from contact surfaces before testing. For uneven parts, use a height gauge to map the marking area and adjust focus by location. Rotate the part 180 degrees and repeat the test. If the error follows the part, positioning is likely responsible; if it stays with the machine, inspect the laser path. I once trusted a clean-looking fixture too quickly, and the real fault was a worn locating pin. A second measurement would have prevented the rework.
Crooked laser marking often starts with a calibration problem, not defective design software. Before changing digital settings, inspect the machine’s mechanical stability, focal distance, and workpiece position. A loose fixture can make a straight path appear misaligned.
Do not guess. Allow the marking system to reach its normal operating temperature. Then mark a square test grid on an approved calibration target. Measure its width, height, corner angles, and center position. Adjust scale, rotation, skew, and origin only after recording the original values. Small changes are easier to verify.
Check the optical path from the source to the focusing lens. The beam should remain centered through the beam expander, apertures, and lens holder. Inspect mirrors and lenses for dust, scratches, or shifted mounts. Even a slight angular error can move the mark significantly across a large field. Use suitable alignment tools and follow the equipment’s safety procedures.
Test again. Use several pattern sizes and positions. Repeat the test after moving the fixture. A common mistake is correcting optical distortion with software alone. That may improve one corner while damaging another. I have found that careful mechanical alignment usually produces more reliable results than aggressive parameter changes. Lock each adjusted mount, save the verified settings, and record the date, temperature, lens position, and test measurements. Perfect once is not enough.
Crooked laser marking often begins with software settings, not the laser head. Check the design rotation, work-area origin, and X-Y scaling values. A small origin offset can turn a straight logo into a visibly slanted mark. I usually load a simple square and crosshair before testing real artwork. The test should match the material, focus height, and fixture position used in production. A perfect preview can still fail.
Adjust one parameter at a time. Record the original values before changing rotation, backlash compensation, or coordinate correction. Mark a 50-millimeter square, then measure both diagonals with a calibrated ruler or digital caliper. Unequal diagonals indicate skew, while equal but incorrect lengths suggest scaling errors. Repeat the test three times. One result can mislead you. I once corrected rotation when the real problem was a loose fixture, so physical inspection still matters.
Tips: Use a low-power test grid to protect the workpiece. Check horizontal and vertical lines separately. Keep the same origin for every sample. If marks drift after repeated jobs, inspect belts, rails, and mounting screws. Save a dated parameter file after each verified adjustment. Leave a small tolerance note for future operators, because materials can expand or shift slightly. Recheck accuracy after cleaning or moving the machine. Calibration is never completely permanent.
How to Fix Crooked Laser Marking Alignment in 2026?
Prevent Future Alignment Errors Through Routine Maintenance
Crooked laser marking often starts with small maintenance problems. Dust on the focusing lens can shift the beam’s visible position. Loose fixtures may also move during repeated production cycles. Check the lens, worktable, clamps, and enclosure before each shift. Use a clean, lint-free cloth and approved cleaning solution. Never touch the optical surface with bare fingers.
Keep the check practical. Mark a small square test pattern on a sample piece. Measure its corners with a calibrated ruler or vision system. Compare the pattern with the programmed coordinates. If the error changes across the work area, inspect the table, rails, and mounting hardware. If the error stays constant, review the focus height and alignment settings. Temperature changes and floor vibration deserve attention too.
I once saw a clean lens fail to solve a crooked mark. The real problem was a slightly loose fixture. That mistake changed our maintenance checklist. Record every inspection, adjustment, and calibration result. Include the operator, date, material, and test pattern used. Review these records weekly for repeating drift. A scheduled check can still be incomplete when one item gets rushed. Replace worn clamps and damaged guides before they affect production. Have qualified technicians verify major alignment corrections with documented measurements.
| Inspection Area | Typical Alignment Symptom | Recommended Control Limit | Inspection Method | Corrective Action | Preventive Maintenance Frequency |
|---|---|---|---|---|---|
| Fixture and Workpiece Seating | The marking is consistently offset or rotated on every part. | Workpiece movement should remain below 0.10 mm during marking. | Check the fixture, locating pins, clamps, and reference edges with a calibrated gauge. | Remove debris, tighten fasteners, replace worn locating elements, and reseat the workpiece. | Before each production shift and after fixture changes. |
| Galvo Scanner or Motion-Axis Squareness | Horizontal and vertical features appear skewed or form a parallelogram. | Maintain measured squareness within the equipment manufacturer's specified tolerance. | Mark a calibrated square test pattern and measure both diagonals with a calibrated optical or mechanical measuring tool. | Inspect mounting hardware, correct mechanical movement, and repeat the coordinate calibration. | Monthly or after relocation, impact, or major service. |
| Lens and Protective Window Condition | The mark has uneven focus, distorted edges, or position changes across the field. | Optical surfaces should be free of visible dust, residue, scratches, and coating damage. | Use angled white light and inspect with a lint-free optical inspection method. | Clean with approved optical materials; replace damaged optics and recalibrate the marking field. | Inspect weekly; clean when contamination is visible or process quality declines. |
| Focus Height and Z-Axis Position | One side of the marking is sharper or wider than the other side. | Maintain the programmed focal distance within the system's specified working range. | Verify height with a calibrated gauge or focus-finding procedure at multiple points on the work surface. | Level the work surface, correct Z-axis positioning, and confirm the focal plane with a test mark. | At setup, after material changes, and whenever mark width changes. |
| Calibration Grid and Field Mapping | Alignment is correct near the center but increasingly inaccurate toward the edges. | Position error should remain within the approved process tolerance across the complete marking field. | Run a multi-point grid test and compare measured coordinates with programmed coordinates. | Apply the correct field-calibration file, verify lens configuration, and repeat the grid test. | Quarterly and after lens replacement, software changes, or mechanical adjustment. |
| Software Coordinate Settings | The design appears mirrored, rotated, scaled incorrectly, or shifted from the reference position. | Coordinate origin, rotation, scale, and correction file must match the approved setup record. | Compare current job parameters with the controlled production setup and backup configuration. | Restore verified parameters, lock approved settings, and document any authorized changes. | Verify at every job change and after software updates. |
| Vibration and Mechanical Stability | The mark contains doubled edges, waviness, or inconsistent line placement. | No visible movement should occur at the marking head, fixture, or work surface during operation. | Inspect mounts and fasteners; observe the test mark at low magnification during operation. | Tighten mounting hardware, isolate vibration sources, and check nearby motors or moving equipment. | Monthly and whenever doubled or wavy marks are reported. |
| Thermal Drift | Alignment is acceptable when cold but shifts after extended operation. | Allow the system to reach its normal operating temperature before final calibration approval. | Record test-pattern position at startup and at regular operating intervals. | Check cooling, airflow, mounting stress, and temperature variation; recalibrate after stabilization. | Monitor each shift; perform a formal review monthly. |
| Reference Test Pattern | Small alignment errors are discovered only after production parts are completed. | The approved test pattern must meet documented position, size, angle, and line-quality limits. | Run the pattern on a stable reference sample and record results in the maintenance log. | Stop production, identify the first failed check, correct the cause, and approve a new reference mark. | At startup, after maintenance, and at defined quality checkpoints. |
| Maintenance Documentation | The same alignment error returns after temporary corrections. | Every calibration, cleaning activity, parameter change, and failed check should be traceable. | Review maintenance records, calibration results, operator notes, and recurring defect trends. | Use a controlled checklist, assign corrective actions, and verify effectiveness after completion. | Update immediately after each maintenance or alignment event. |
Small alignment errors often cause crooked marks. Check the laser head, fixture, and workpiece together. Do not blame software too quickly.
Place a calibrated test plate beneath the head. Mark a small grid at several heights. Uneven widening may indicate lens, focus, or head stability problems.
A loose clamp can move slightly during production. Letters may then appear slanted. Tighten contact points evenly and check the base with a machinist’s level.
Keep the workpiece flat against the same datum. Remove chips, oil, and burrs first. Locating pins or hard stops improve repeatability.
Rotate the workpiece 180 degrees and repeat the test. If the error follows the part, positioning is likely responsible. If it stays fixed, inspect the machine path.
Let the system reach normal operating temperature. Mark a square grid on an approved calibration target. Measure width, height, corner angles, and center position.
Software can adjust scale, rotation, skew, and origin. Record original values before changing them. Mechanical alignment usually provides a more reliable foundation.
Inspect the lens, table, clamps, and enclosure before each shift. Use a lint-free cloth and approved cleaning solution. Never touch optical surfaces directly.
Record the operator, date, material, temperature, lens position, and test pattern. Save verified settings and measurements. Test twice.
Do not assume a clean fixture is accurate. A worn locating pin can cause rework. One inspection may still be incomplete, especially after vibration or heating.
Crooked laser marking alignment can result from several factors, including an unstable fixture, an uneven workpiece, incorrect lens positioning, vibration, or a shifted optical path. If you are asking, “why does my laser marking alignment look crooked,” begin by inspecting the laser head, mounting structure, fixture, and workpiece position. Confirm that the surface is clean, level, and securely held before making adjustments.
Next, calibrate the marking system and carefully align the optical path according to the equipment’s operating instructions. Review software settings such as scale, rotation, focus, and correction parameters, then run a test pattern to compare the actual mark with the intended design. To prevent future errors, regularly clean optical components, check fasteners and fixtures, verify focus, and inspect calibration accuracy. Recording maintenance results and correcting small alignment changes early can help maintain consistent, straight, and accurate laser markings over time.
Jigsaw Machine